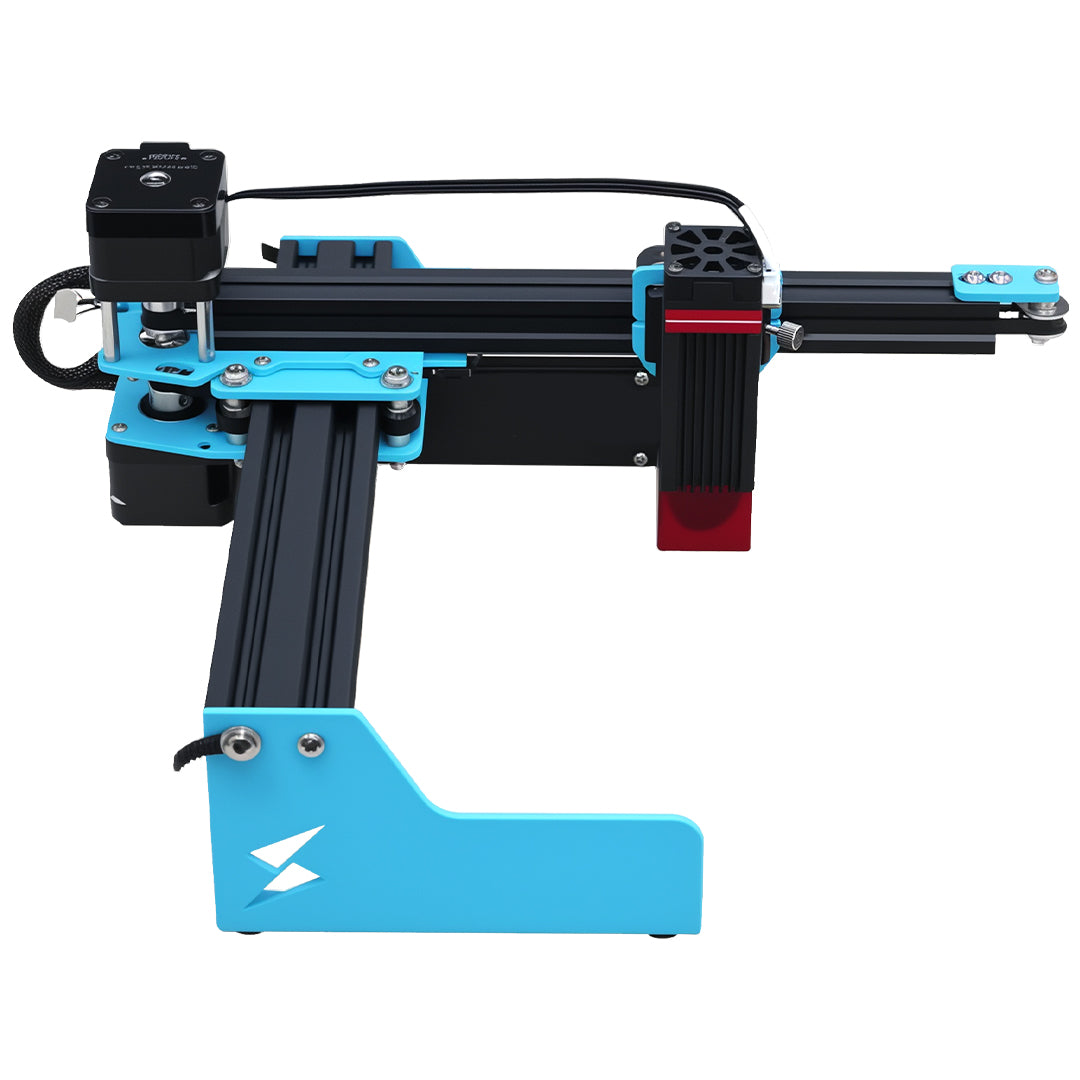


For a single wrench, a hand engraving pen may be a perfectly reasonable way to add an owner name. For a fleet of tools with legible serials, company logos and a documented rework process, the decision changes. Searchers comparing a “metal engraving pen” with a “laser metal engraving machine” need to look at the number of parts, required appearance and who is accountable for data. TYVOK P2 Ultra is a compact 20W 1064 nm fiber option to test when the job is repeatable metal identification.

Official P2 Ultra product image. A tool-ID mark should be tested on the tool's actual finish.
Decide what the mark must do
Is the goal to discourage casual mix-ups, support inventory scans, or keep an identifier readable through service life? A hand-inscribed name may satisfy the first goal. A small, consistent company logo and serial on fifty identical parts call for an approved file and repeatable placement. Do not promise permanent traceability without testing wear, cleaning and any relevant customer standard. The tool's alloy, plating, coating and heat-treated zone also matter.
Mark a location that will not be ground, gripped, obscured by a socket or covered by a replacement handle. Ask the tool manufacturer or customer if marking a stressed or safety-critical area is prohibited. A marking shop should not independently declare a structural tool safe after changing its surface. The same caution applies to deep engraving: remove only what has been approved for that part.
Compare effort per accepted tool
For the pen, count individual layout and operator variation. One label on one personal tool can be fast and inexpensive. For a repeated laser job, count artwork and fixture setup first, then time each loaded, marked, cleaned and inspected tool. The P2 Ultra official product page lists a 150 × 150 mm marking field and red-light positioning. That is useful for repeat placement, but a different tool geometry still needs a secure fixture and its own focus check.
| Decision factor | Hand engraving pen | P2 Ultra fiber workflow |
|---|---|---|
| One-off setup | Usually simple | Artwork, test and safe setup required |
| Variable serials | Manual transcription risk | File and data controls still required |
| Repeat placement | Depends on operator and guide | Can use a qualified fixture |
| Fine logo | Harder to reproduce consistently | Testable digital artwork |
| Capital cost | Lower typical entry | Equipment, extraction and station costs |
The table is a process comparison, not a promise that the laser always wins. A heavily textured or awkward tool may be difficult to fixture. A single emergency replacement in the field may be better handled with an approved manual method. A large order of identical tags for toolboxes may be easier to mark off the tools entirely.
Proof the laser route on a real tool
Use a sacrificial or customer-approved spare. Clean and document the surface. Place the actual text and logo at final size, then test a modest mark using the official starter guidance for the material. Inspect under worksite lighting and after the cleaning method the tool normally sees. Check that the ID is visible without needing a perfect photo angle. If serialized, reconcile the physical tool and the source list, and record any rejected identifier.
Before batching, run a first piece in the final fixture. Stop after a tool change, coating lot change or artwork revision. Keep unmarked, marked and inspected tools separate to avoid duplicate or missing serials. A digital design solves repeatable typography; it does not solve poor data control by itself.
Test identification after real use
Make the wear test reflect the tool's actual environment. A mechanic's wrench may meet oil, wiping and drawer abrasion; a showroom sample might not. Record the baseline legibility, run the agreed handling steps, then inspect again under worksite light. If a reader must scan a code, use that reader after the wear test as well. Keep manual and laser examples on comparable tools from the same finish lot. This is fairer than comparing a freshly marked laser sample with an old hand-inscribed tool. Where the part is safety critical, involve the owner or manufacturer in approving both the mark location and test method before modifying it.
Buying threshold
Estimate the expected number of accepted marked tools per month, the labor saved over manual marking and the new station costs. Include extraction, a Windows computer for current TyvokWorks support, fixture material and spare-tool tests. If the program needs formal part marking verification, budget for that inspection as well. Review P2 Ultra pricing and package contents against this volume, not against a single engraved sample.
Is a pen always the cheap option? For one-off identification it can be; repeated, controlled serial work has additional labor and error costs.
Can P2 Ultra mark a safety-critical tool anywhere? No. The owner or manufacturer must approve location and mark requirements.
What proves the choice? Same-tool samples, a timed process and inspection after expected handling. See current P2 Ultra purchase options after that comparison.