

Two plywood sheets with the same printed thickness can cut differently. One may separate cleanly while another has a glue-heavy region, an internal void, or a veneer defect that appears only after parts are removed. For an X1S Pro kit or sign order, qualify the exact plywood grade and supplier lot, inspect the first sheet's edges and parts, and set an acceptance rule before running the entire stack. Increasing laser power to overcome one bad spot may overburn the rest of the sheet.

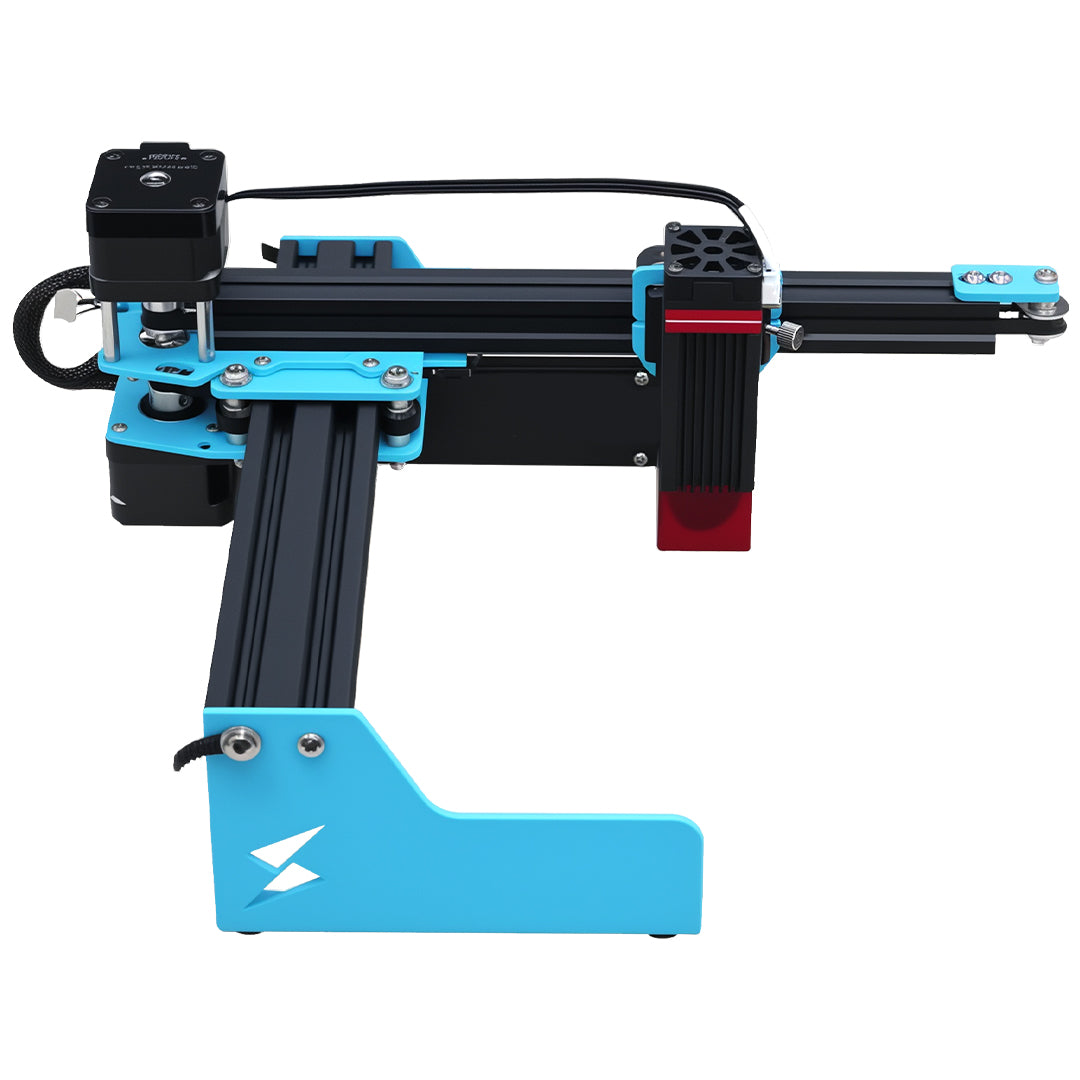
TYVOK X1S Pro product image; inspect the actual plywood core and cut parts before a batch.
Buy for laser processing, not just dimensions
Ask for the wood species, layer construction, glue system, and grade. Look for plywood offered and documented for laser use rather than assuming all craft plywood is equivalent. Trotec's wood guidance points out that glue and surface texture affect laser results; that observation is a material-selection warning, not a preset for TYVOK. Record the supplier, lot, nominal thickness, measured thickness at several positions, and visible face grade. Reject sheets with warping or surface defects that cross critical artwork before they reach the machine.
The TYVOK X1S Pro comes in selected workspace and module variants. Confirm the current configuration and test the actual material with that module. A power rating cannot tell you whether a particular adhesive layer will cut cleanly or whether the edge color meets the customer's standard. If the plywood composition is unknown or the adhesive is unsuitable for laser work, pause until the supplier provides a safer, identified stock.
Map defects against the parts, not against the sheet alone
For a kit, a void through a tab or slot may make a part unusable even if it sits far from the visible face. For a sign, a pale patch across the headline may be unacceptable while a small back-side knot is hidden after mounting. Lay out the actual part outlines over a photographed sheet and mark critical zones. Keep a sheet ID linked to the nesting file. If the design contains paired left and right parts, preserve their face orientation and grain direction; the matched-panel guide explains the presentation issue for adjacent boards.
| Defect or variation | First-piece check | Release choice |
|---|---|---|
| Visible face void or patch | Compare with customer finish standard | Move part or reject sheet |
| Hidden core void at tab | Fit and flex test the actual part | Reject weak part |
| Glue-heavy cut section | Inspect separation and edge char | Change stock or qualify a new process |
| Thickness variation | Test joint clearance | Split lot or adjust approved fit |
Do not rely on a single straight test line. Place a small test pattern in representative sheet areas and include a corner, narrow slot, and long cut from the real design. Record where the cut succeeds and fails. If a single region will not separate, examine the stock before adding more passes. Repeating energy across the entire sheet can deepen charring, widen kerf, or increase fire risk without fixing a void or dense glue line. Use active supervision, effective exhaust, clean supports, and fire readiness. Stop for flame, unstable stock, or smoke behavior beyond the qualified sample.
Set an acceptance standard for the paid item
Show the customer a physical edge and face sample after the planned sanding or finish. Agree on permissible char, visible knots, small voids, and the fit of interlocking parts. A promotional image of perfect birch does not describe the actual lot. Measure critical slots and tabs after cutting; a nominal 3 mm design is not a substitute for the actual board thickness. Count accepted parts, not only cut paths. Keep rejected pieces separate so they do not accidentally enter a kit.
For multi-sheet runs, inspect the first sheet fully and sample subsequent sheets by lot and position. Recheck after a sheet change, refocus, support adjustment, or tool path revision. Label packed kits with their part count and version. If a customer reports a fit failure later, the sheet ID and accepted sample let you investigate whether the cause was design clearance, plywood variation, or assembly. Without that record, another operator may simply increase power and create a new problem.
Know when to change the material
If a lot repeatedly exposes internal gaps, requires excessive cleanup, or cannot meet the edge specification, stop the run and qualify better plywood or another appropriate material. Explain the effect on cost and lead time before substituting stock. Wood is a natural and manufactured material with variation; an honest acceptance standard protects the customer and the shop more than a claim that every sheet can be made identical by changing a laser setting.
Can I fix an internal void with a second pass? No. A void is a material defect; another pass may worsen nearby edges.
Is nominal thickness enough for press-fit parts? No. Measure the actual lot and test assembled parts.
Should I cut all sheets after one small proof? Inspect a full first sheet and continue with a documented sampling plan that catches lot changes.
Match the machine to accepted plywood output
Review X1S Pro configurations and buy options after testing your supplier lot and calculating accepted parts per sheet.